 English
 Deutsch
 Français
 Español
 Nederlands
 Polski
 Italiano
 Română
 Türkçe
 Português
Diagnostics and inspection
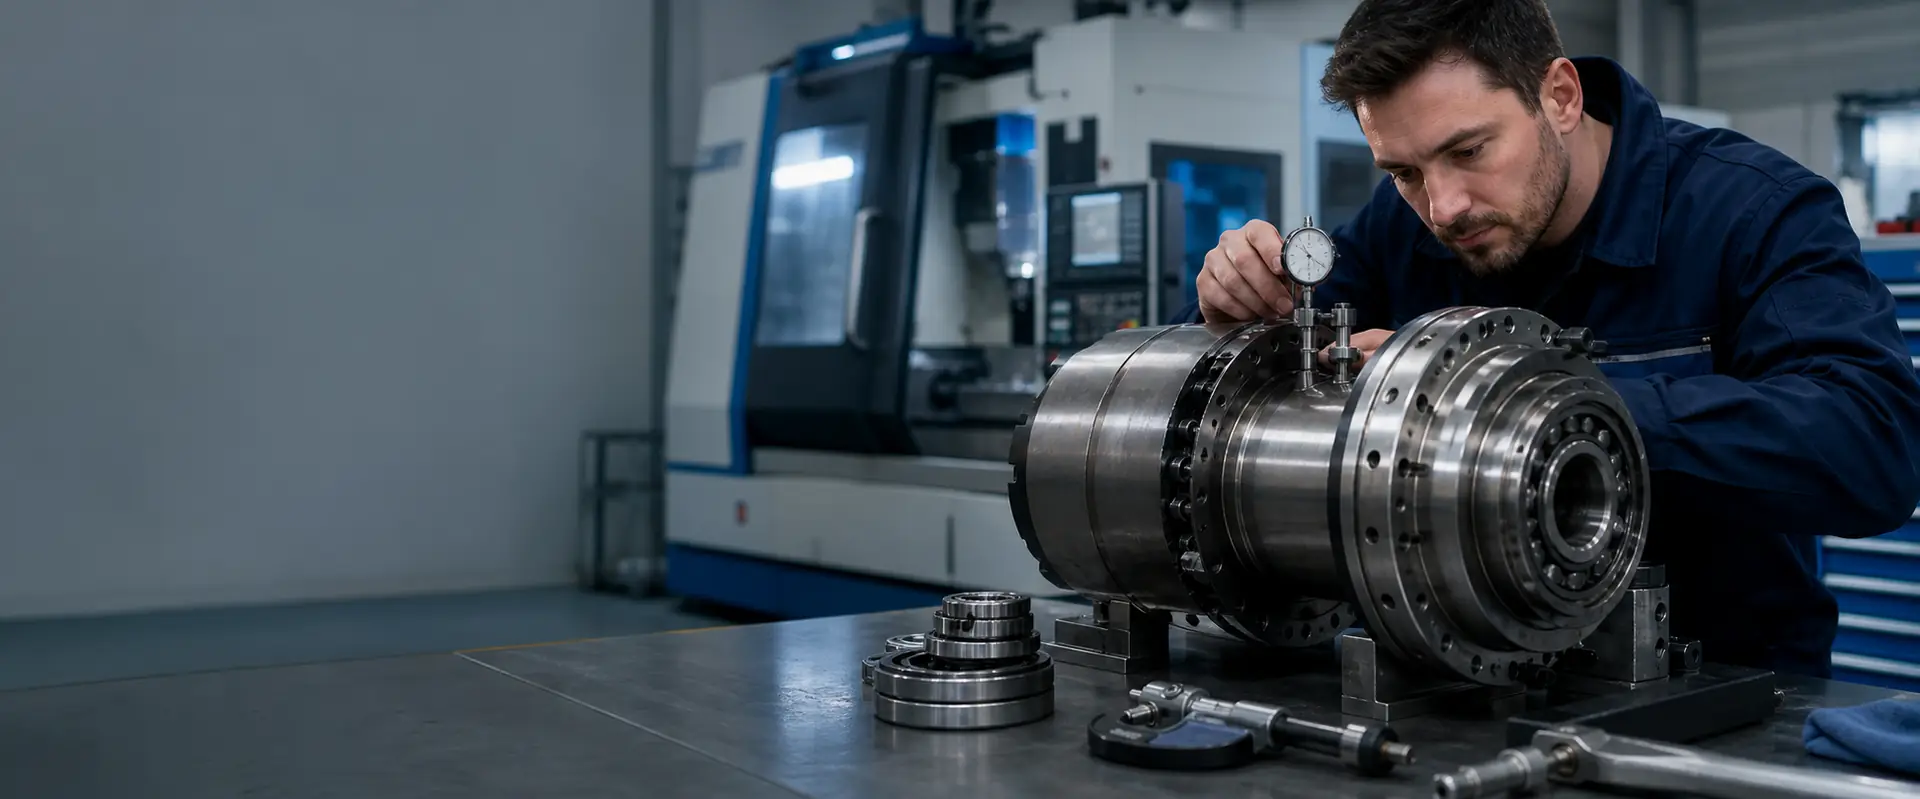
Chargeable incoming inspection: runout, geometry, vibration, insulation resistance and teardown findings, written up with measured values and photographs.
Services
Most spindles that reach us need several of these operations at once, so we normally quote a rebuild rather than a single item off a price list. The pages below explain each operation on its own: what it involves, when it is worth doing, and what we need from you before we can put a figure on it.
Directory
Eight workshop operations, one page each, ordered roughly the way a spindle passes through the workshop — followed by four services around the repair: preventive maintenance, exchange and loaner spindles, retrofit and upgrade, and emergency support. Every step ends with a measurement that goes into the test report, so you can see what was done and which values the spindle reached. The four additional services can be combined with a repair or arranged on their own.
Chargeable incoming inspection: runout, geometry, vibration, insulation resistance and teardown findings, written up with measured values and photographs.
Matched angular contact bearing sets, preload set for the spindle design, seats measured, and grease or oil-air lubrication restored.
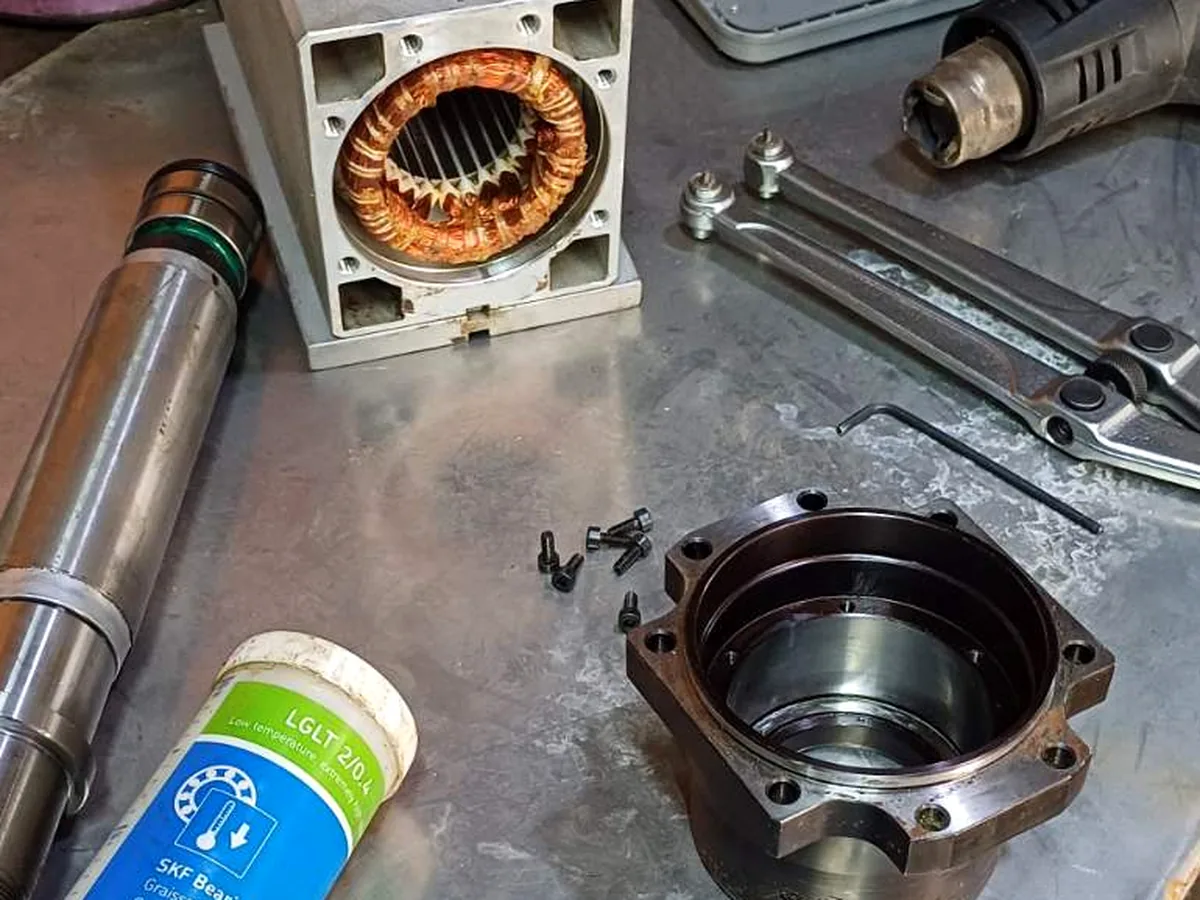
Rotor and stator rewinding for motor spindles: insulation and surge testing, rewinding to recorded data, impregnation and a measured run-in.
Two-plane balancing of the rotating assembly, checked at operating speed, with residual unbalance and run-in values in a written test report.
Rotary encoders and speed sensors: signal measurement, contamination and cable faults, replacement and alignment, with drive electronics diagnosed and reported rather than repaired.
Worn bearing seats measured for geometry, bores sleeved and reground to size where the material allows, with coolant channels and seal seats restored.
HSK, BT, SK and CAT seats reground in the assembled spindle where the design allows, referenced to the bearing journals and checked with a gauge.
Removal, refitting, alignment, commissioning and vibration measurement at your machine, arranged technically in advance from the workshop in Germany.
Planned checks of runout, vibration, temperature, clamping force and sealing air, compared over time so a rebuild can be scheduled before a failure.
Rebuilt exchange units or loaner spindles to bridge the repair time, in individual cases and only where a suitable unit is available and agreed in advance.
Hybrid ceramic bearings, better sealing, sealing air, improved cooling and finer balancing, fitted during a rebuild where technically sensible.
Urgent spindle failures prioritised during business hours: quick first assessment, help with removal and shipping, and a realistic timeline.
Not listed
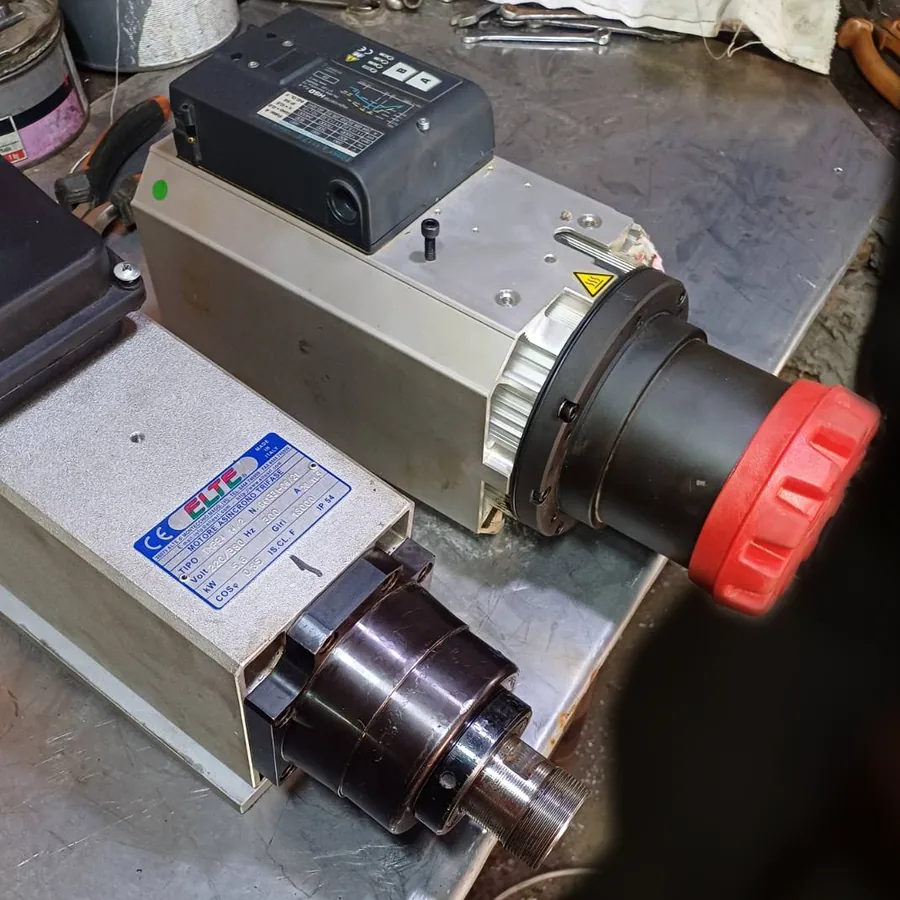
That is normal, and it is our job rather than yours. Describe the symptom — the noise, the finish on the part, the alarm code — send photographs of the nameplate, and we will tell you what the spindle most likely needs and what it will take to confirm it. If the description and photos are not enough to find the cause, a paid inspection in the workshop is the usual first step, and its findings form the basis of the quotation.
Quote
Tell us the machine model, the spindle type and what the machine is doing wrong. We come back with an initial assessment and a written quote before any work begins.