 English
 Deutsch
 Français
 Español
 Nederlands
 Polski
 Italiano
 Română
 Türkçe
 Português
 Čeština
 Magyar
 Svenska
Machine type · turning
CNC Lathe and Turning Centre Spindle Repair
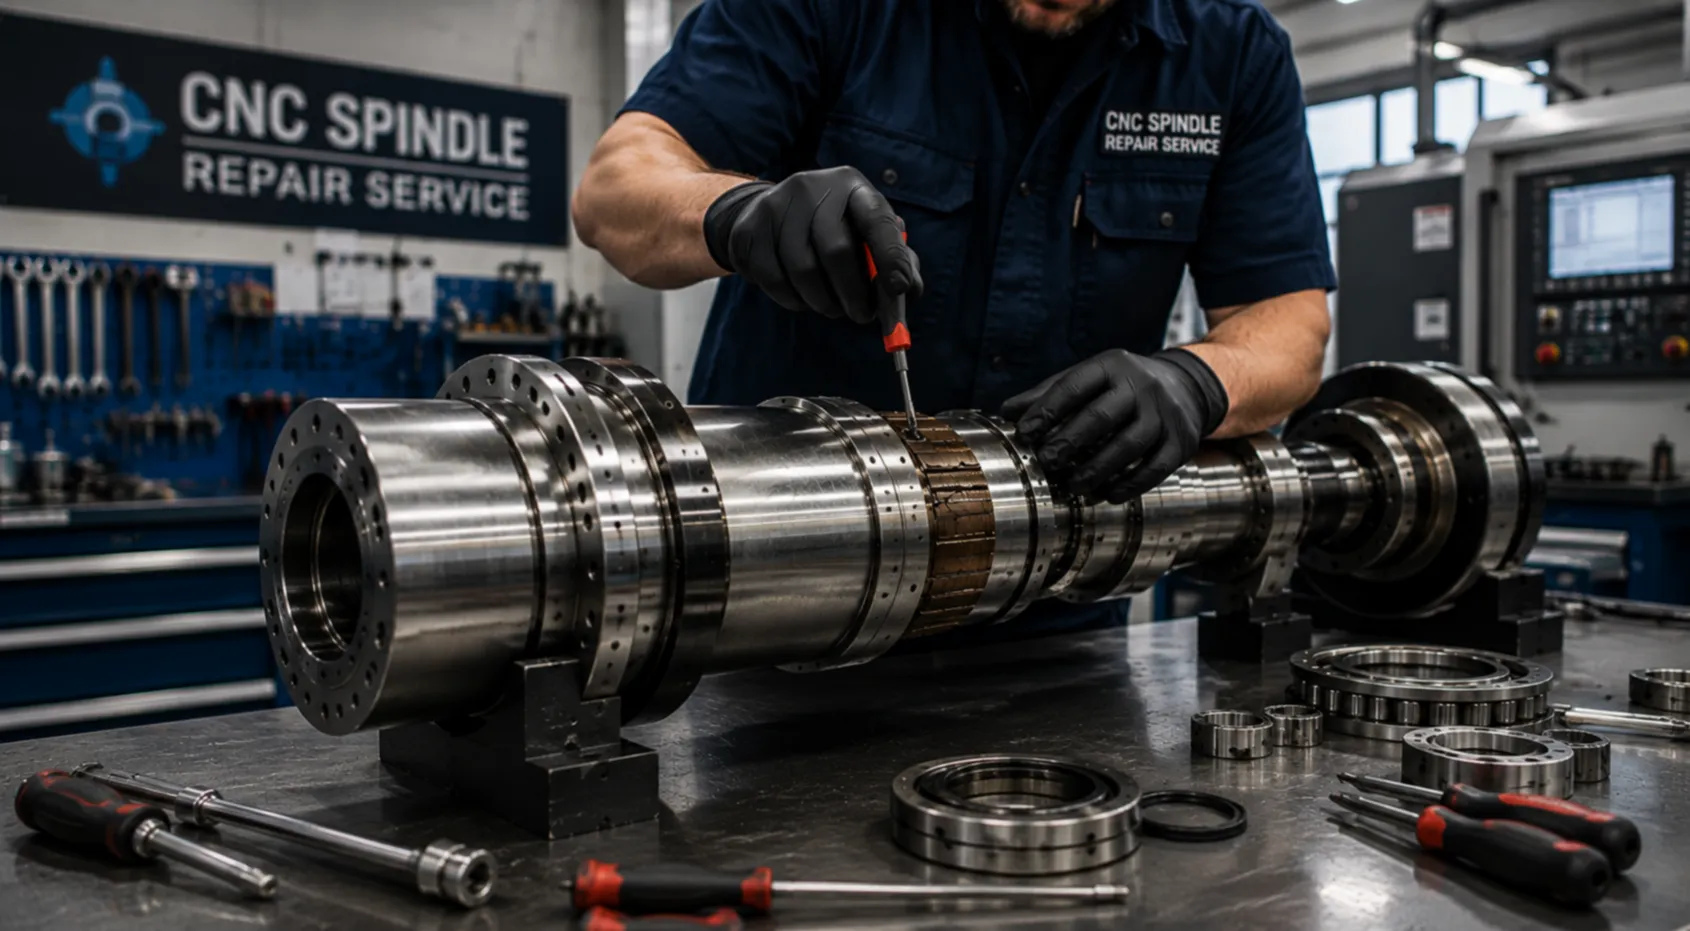
A lathe spindle carries the chuck, the workpiece and the hydraulic clamping cylinder, takes high radial loads and often feeds bar stock through its bore. In our workshop in Sankt Augustin, Germany, we repair main spindles, sub-spindles and driven-tool units of CNC lathes and turning centres — from simple two-axis lathes to machines with C-axis and live tooling.

Inside the unit
How a CNC lathe spindle is built
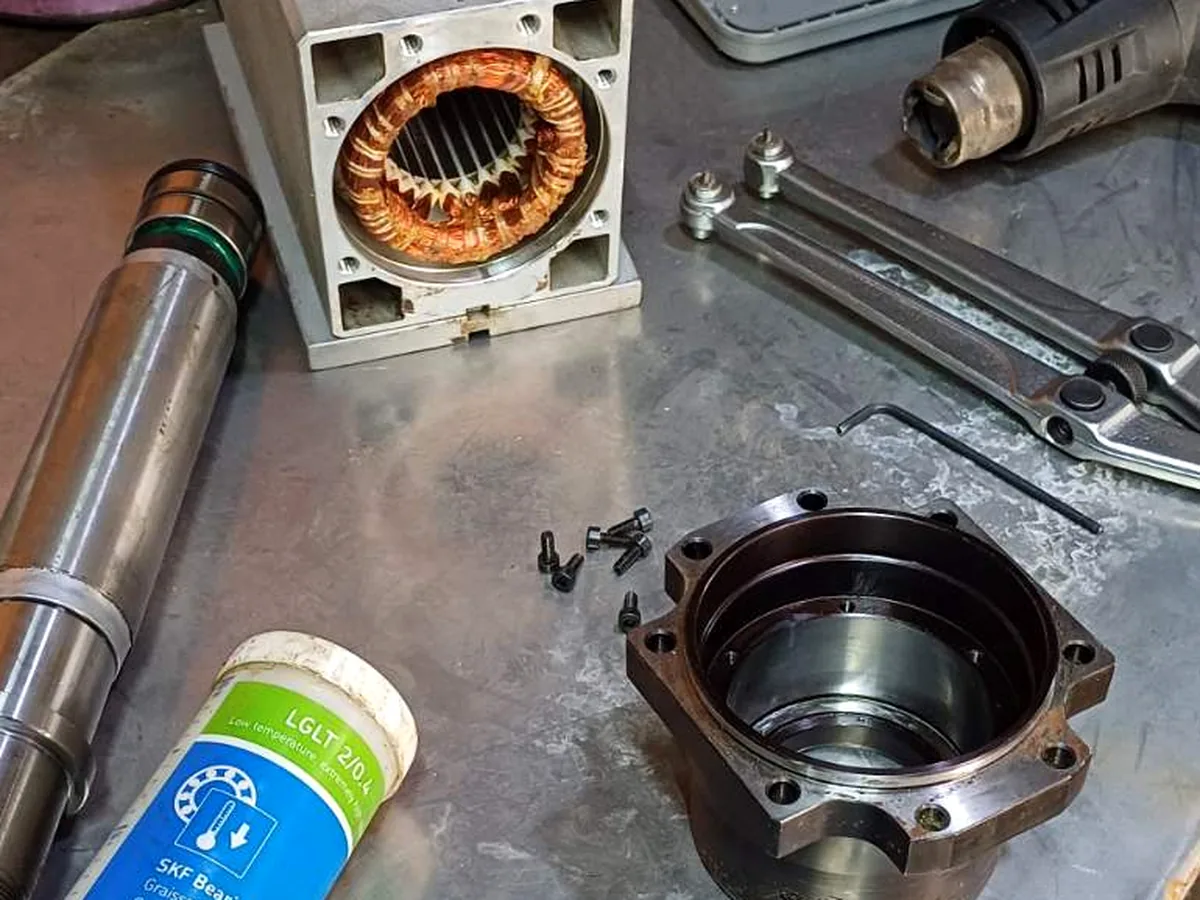
The main spindle is a hollow shaft on double- or triple-row bearing arrangements, with a chuck flange at the front and a rotating hydraulic cylinder at the rear. A draw tube runs through the shaft and transfers the cylinder force to the chuck jaws; the bore sets the maximum bar diameter. An encoder or sensor on the shaft handles threading, orientation and the C-axis.
For an initial assessment, send the machine model and photos of the spindle flange and the motor plate — from them we identify the design and plan the work.
- Chuck flange: A2-5, A2-6, A2-8 and other sizes
- Drive: belt from a separate motor, or built-in motor
- Hydraulic chuck cylinder, draw tube, bar bore
- C-axis, encoder, spindle brake or lock
Designs
Lathe spindles we repair
A CNC lathe can carry several spindle units of different design. Each one is repaired by its own procedure and tested on the bench separately.
Belt-driven main spindle
The most common layout: a separate spindle motor drives through a poly-V or toothed belt. We rebuild the bearing arrangement, fits and pulley, and set the belt tension.
Built-in motor spindle
The motor rotor sits directly on the spindle shaft. Besides the mechanics, we test the stator, winding insulation and sensors, and carry out rewinding where needed.
Sub-spindle (counter spindle)
The second spindle for machining the back of the part. Similar in design to the main spindle but more compact; we repair it together with its cylinder and sensors.
Driven tools in the turret
Spindles of live-tool units for milling and drilling on a turning centre. We replace bearings and seals and check gear mesh and runout.
Symptoms
Common faults on lathe spindles
A lathe spindle is the first to react to an unbalanced workpiece, jaw impacts and running at full power. These are the symptoms we are asked about most often.
Bearing noise and heat
Humming at speed, a hot front bearing, rising motor current. Bearings are replaced as a set with the correct preload.
Runout at the chuck face
Oval or lobed parts, unstable dimensions. We measure the runout of the flange and centring spigot and restore the locating surfaces.
Vibration and chatter
Chatter marks on the surface, especially at long overhangs. We look for the cause in the bearings, unbalance and stiffness and carry out balancing.
Belt slip
Speed drops under load, the belt squeals. We check the pulleys, tension and belt condition and replace the set.
Cylinder and draw tube leaks
Loss of clamping pressure, oil on the headstock. We repair the chuck cylinder, its seals and the draw tube.
Encoder, C-axis, motor
Threading and orientation faults, C-axis backlash, drive alarms. We check the encoder, the locking mechanism and the motor winding.
Process
How we repair a lathe spindle
- We identify the design from the machine model and photos and agree the scope of diagnostics.
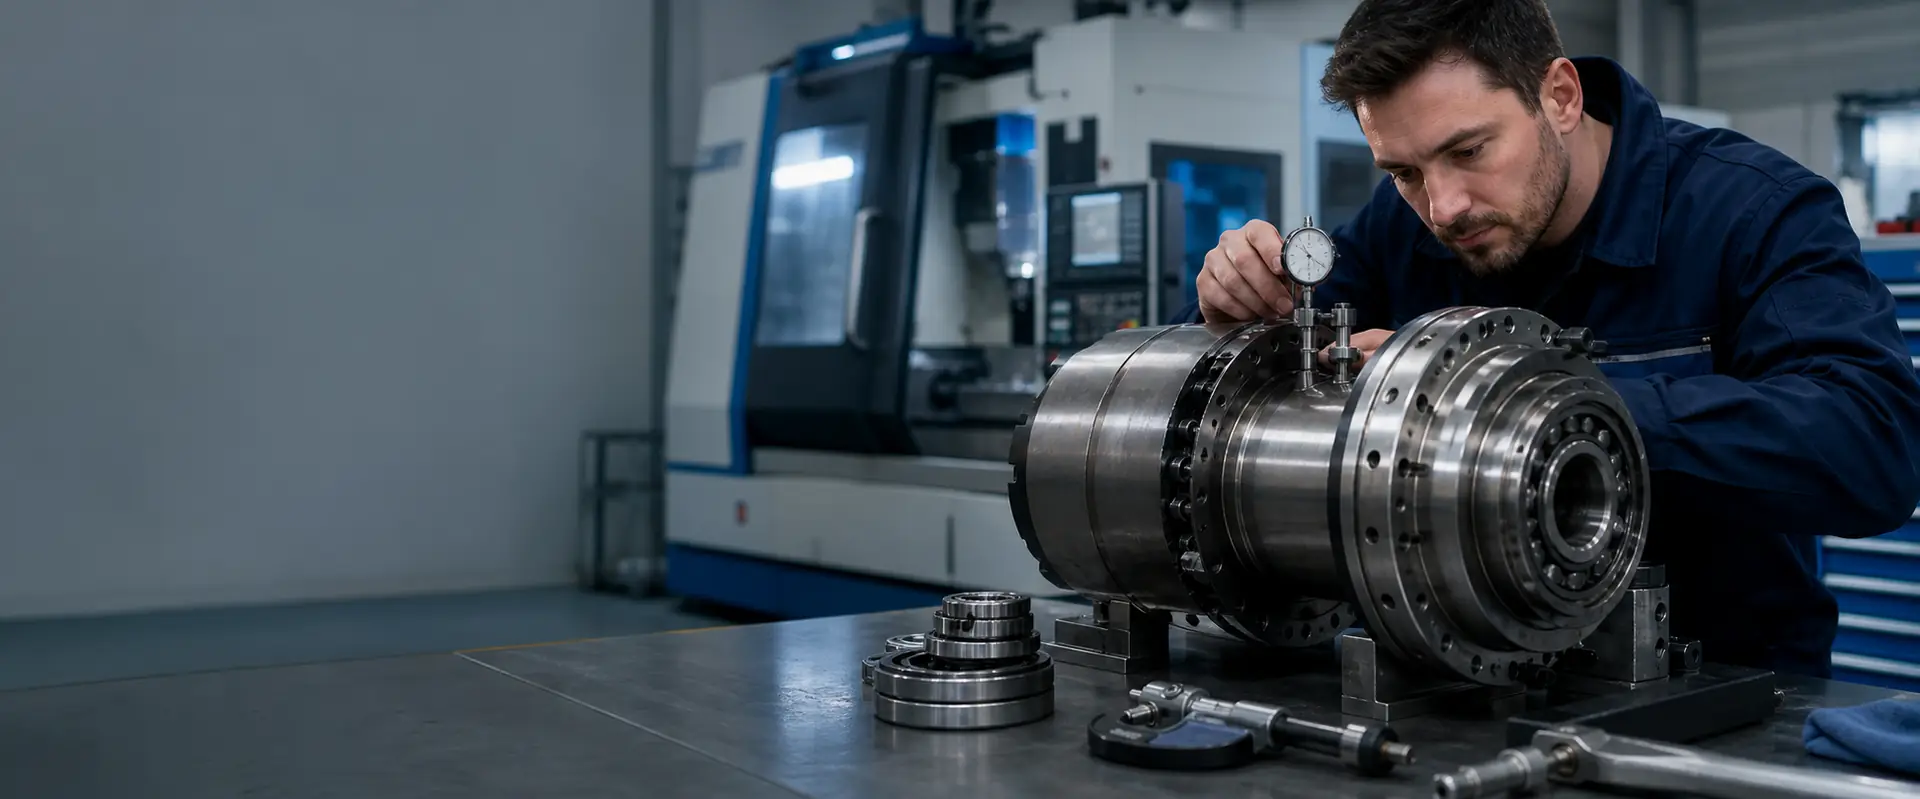
- The spindle is stripped and the shaft, fits, flange and draw tube are measured.
- You receive a written quotation with inspection photos; work starts once you approve it.
- Bearings and seals are replaced, sourced new from the European market.
- The unit is assembled, the bearing preload is set, and it is balanced and run in with temperature and runout monitoring.
- It goes back to you with a measurement report; we can also fit it on site through our on-site service.
Lathe brands and spindle motors
Lathe spindles reach us most often from Okuma, Mazak, Doosan, Haas and DMG Mori machines; details for each brand are on its own page.
Main drive motors on lathes are mostly Fanuc, Siemens or Mitsubishi; we repair them together with the spindle or separately.
Questions
Lathe spindle repair — frequently asked
The spindle alone is enough; the chuck and cylinder are removed before shipping. If you suspect a leaking cylinder or draw tube, send them too and we check everything together.
Measure the runout at the face and centring spigot of the flange with the chuck removed. If it is within the machine's tolerance, the cause is usually the chuck or jaws; we help you work it out from photos and readings.
Yes. Sub-spindles and driven-tool units are repaired the same way as main spindles: inspection, bearing replacement and testing on the bench.
The machine model, photos of the spindle flange and motor plate, and a description of the symptoms: noise, heat, runout, chatter or C-axis alarms.
By courier or freight forwarder, in rigid packaging with the flange protected. Within the EU there is no customs paperwork; for other countries we help with the export and return documents.
Send us photos of your lathe spindle
Give us the machine model, the flange type and the symptoms — we prepare an initial assessment and a written quote before any work begins.
Scope
Our spindle services
Every operation below is done in our own workshop in Germany. Follow a link for what it involves and what we need from you.
Machine brand
Machine brands
We are independent and work with spindles of every builder. These are the makes whose spindles come across the bench most often.